Inch-Pounds, Not Ugga-Duggas: Staging a Valve Body So the Casting Stays Flat

Photo by Photo by Tekton on Unsplash on Unsplash
Everybody has gotten away with a pan. Snug it down in a circle with a 3/8 ratchet, wipe the drip, and it usually seals. That habit follows people into the valve body, and that's where it stops being harmless. A transmission pan is a stamped lid over a big open sump. A valve body is a machined casting with hydraulic channels routed millimeters beneath the bolt bosses. Clamp it unevenly and you don't get a leak you can see. You get cross-leaks you can't find.
The Casting Is the Circuit
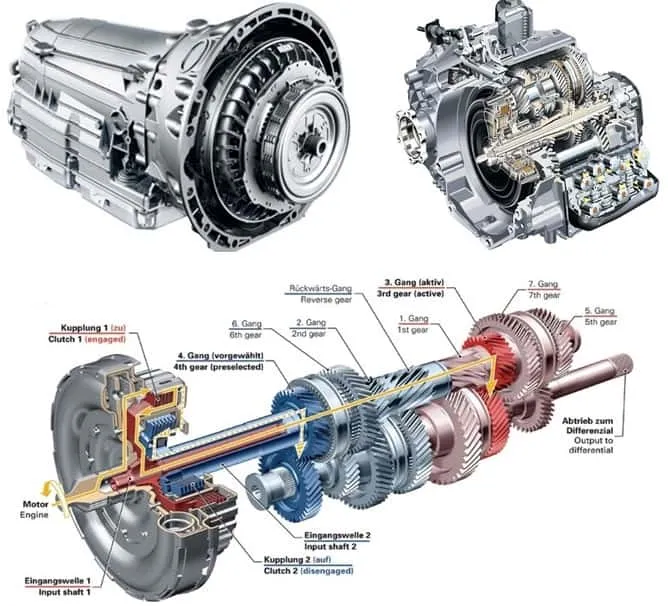
Look at the matte face of a 4L60E or a 6L80 valve body and you're looking at the lid of a plumbing maze. Separator plate on one side, case on the other. Every spool valve in that casting needs its bore to stay round, and every channel needs the plate to stay pressed flat against it. Bolt torque is how that happens.
Here's the failure mode. Over-torque one corner and the casting deflects between bolts. The gasket crushes unevenly — tight where the bolt is, barely touched a couple inches away. Fluid migrates from a 90 psi channel into the low-pressure channel next door, and suddenly you're diagnosing a bind-up in second gear that looks exactly like a solenoid. Or the bore distorts just enough that a spool valve hangs when the fluid is cold.
There's a second trap that bites experienced hands: bolt length. On several domestic units, one or two fasteners share a casting with a shorter cousin, and swapping them puts a long bolt into a blind hole. It bottoms out, and the next quarter turn drives the tip into a channel on the far side of the casting. The bolt feels fine. The circuit is now vented to atmosphere.
Read the Pattern Before You Touch the Wrench
Most OEM service info publishes a numbered bolt pattern, and it exists for a reason. The general shape is center-outward in a spiral or X, alternating sides as you go — the goal is to bring the whole face down evenly instead of pivoting it around one corner. If your manual has a diagram with numbers on it, those numbers are the order. Not a suggestion, not a starting point.
If you don't have a diagram, the safe default is: center bolts first, then work outward, alternating across the casting so you're never stacking clamp load on one end.
Three Passes, Always in Inch-Pounds
One pass to full value is how castings get warped. Stage it.
- Pass one: 40 to 50 percent of final spec, in sequence. This is where you're just seating the plate and pulling the gasket down evenly.
- Pass two: 80 percent, same order.
- Pass three: full spec, same order.
- Verification pass: a slow walk back through the sequence at full spec, letting the wrench click rather than adding a nudge. If a bolt moves on this pass, you had uneven clamp load somewhere.
For reference, common domestic valve body-to-case figures land in these neighborhoods — 4L60E and 4L65E around 97 to 115 lb-in, 4L80E a bit higher, 6L80 and 6L90 down around 70 to 80 lb-in, the Ford 4R70W family in the 90 to 110 lb-in range. Treat those as ballpark only and confirm against the service information for the exact unit in your bay. The separator plate and small cover fasteners are frequently a separate, lower spec — often in the 35 to 55 lb-in range. Those little bolts dish the plate if you lean on them, and a dished plate changes what the valves see.
Use a 1/4-inch drive inch-pound wrench. A 3/8 clicker set to its lowest setting is not an inch-pound instrument — most of them are barely accurate down there, and none of them belong anywhere near a valve body with air behind them.
The Flatness Check Almost Nobody Runs
Before anything goes back on, run a straightedge across the machined face in three directions — long way, short way, and diagonal. Slide a feeler gauge under it. A field rule of thumb for these castings is a couple thousandths across the bolt span; if you can catch 0.003 inch, stop and have a conversation. Do the same on the case side, because a flat valve body bolted to a scarred case face is still a leaker.
Then check for burrs. A single raised ding at a bolt hole holds the entire casting proud of the case by however tall that burr is. A few light passes with a fine oilstone on a flat surface will show you the high spots immediately — they shine while the rest stays dull. Knock them down, clean thoroughly, and re-check.
One more: blow out every blind bolt hole before assembly. Trapped ATF in a blind hole doesn't compress. The bolt acts like a hydraulic ram and can crack the boss before it ever seats.
Bench Checklist
- Correct gasket and plate for the unit, oriented correctly — plates go on one way, and flipping one is a guaranteed no-forward or no-reverse complaint
- Check balls, screens, and accumulator springs accounted for and in the right pockets
- Manual valve indexed to the shift linkage before the body goes home
- Detent spring and roll pin seated
- Solenoid harness pass-through and connector O-ring in place, not pinched
- Bolt lengths sorted and mapped, not scooped out of a coffee can
- Threads clean and dry, no sealant on fasteners that spec dry
- Inch-pound wrench calibrated and in hand
Where People Go Wrong
Impact guns. RTV on a gasket that's designed to go on dry. Reusing a crushed separator plate gasket because it looked okay. Chasing a leak by adding torque instead of finding the cause — that's how a bolt boss cracks. Reassembling the same casting twice in a week after the first attempt didn't fix the complaint.
When to Stop Chasing It
Some castings aren't worth saving. If flatness is out beyond spec, if there's corrosion pitting inside the channels, if a bolt boss is cracked or the threads have already been repaired once, or if the bore wear is in the valve body itself rather than the valves — no gasket, no sequence, and no amount of patience fixes that. The valve body is the bore on plenty of units. A warped or worn one is a hydraulic problem, not a sealing problem.
Do the math honestly. A remanufactured or upgraded unit with a warranty versus your third Saturday on the same casting, plus fluid, plus the risk of a comeback you're eating. If the core is sound, rebuild it right and stage the bolts. If it isn't, send it back and put a known-good piece in the truck.